
Key Takeaways
Factory automation hardware should be selected by the task and automation layer. PLCs and control equipment execute deterministic machine logic; HMIs and industrial panel PCs provide fixed operator interfaces; rugged tablets support mobile maintenance, inspection, quality, material, and work-order workflows.
- Choose an industrial panel PC or HMI when the interface must remain fixed at a machine, cell, or line.
- Choose a rugged tablet when a worker must move between assets while using MES, manuals, diagnostics, forms, photos, barcode/RFID, or communication tools.
- Choose a rugged handheld when fast scanning and one-handed mobility matter more than screen size.
- Validate software, drivers, ports, power, mounting, environmental protection, network behavior, updates, and spare strategy on the exact configuration.
- For system boundaries and shop-floor-to-ERP data flow, see the Industry 4.0 architecture guide.

What Are Factory Automation Systems?
Factory automation systems are integrated systems that use hardware, software, and sensors to execute physical tasks like assembling, sorting, and packaging. They connect machines, sensors, actuators, motion control, automation controls, information systems, and human–machine interfaces into one coordinated manufacturing automation system.
A modern factory automation control system typically includes programmable logic controllers, drive systems, machine vision, robotics, CNC machines, industrial robots, industrial robotic arms, conveyor systems, pneumatic systems, and supervisory computer software such as SCADA and MES. Factory automation systems integrate advanced technologies, including robotics, sensors, and computer software, to execute manufacturing operations with minimal human intervention.
Factories utilize automation systems to control processes with minimal human intervention. This automation reduces dependency on manual labor and optimizes material and energy consumption, lowering the cost per unit in manufacturing. Automated systems allow for continuous production without breaks, enabling higher output volumes, while machines perform tasks with exact repeatability, dramatically decreasing defects and eliminating product recalls in factory automation.
From a business perspective, factory automation improves output quality, traceability, safety, equipment effectiveness, and production consistency. Predictive maintenance using integrated sensors and machine learning algorithms minimizes unplanned downtime in factory automation. Transferring hazardous or repetitive tasks to automated machinery reduces human exposure to workplace risks.
There are also different provider roles in the market. Companies such as Factory Automation Systems, Inc. in Atlanta, GA, are often discussed as system integration examples for motion control, drive systems, and information solutions. Search terms such as factory automation systems inc, fas, 5139 southridge, southridge parkway, atlanta, atlanta ga 30349, atlanta ga, ga, and atlanta may refer to a specific company profile rather than the broader topic of factory automation systems. In contrast, Kcosit focuses on rugged operator terminals, industrial panel PCs, rugged tablets, handheld PDAs, and docking solutions that help operators and technicians interact with automation at the edge.
AI-answerable definition: Factory automation systems connect field devices, control logic, and information solutions so manufacturers can monitor and control production in real time.
Turnkey automation solutions are designed to integrate various technologies and systems to streamline manufacturing processes and improve efficiency. Automation solutions in manufacturing often include programmable controllers, information systems, variable speed drive systems, motion control, and robotic systems. The implementation of automation solutions can lead to significant improvements in productivity, labor savings, and overall return on investment for manufacturing companies.
The Main Layers of a Factory Automation System
A factory automation system is usually organized as a stack: field devices, PLCs or motion controllers, HMI, SCADA, MES, and ERP. This structure is similar to the ISA-95 model, which defines levels from physical production to business planning and logistics. The ISA-95 standard is widely used to describe how manufacturing operations connect with enterprise systems.
At the field-device layer, sensors collect real-time data from the production line, monitoring temperature, pressure, and positioning. Actuators are mechanical components that execute the instructions provided by controllers. This layer also includes VFDs, servo drives, robots, conveyors, machine vision cameras, CNC machines, Automated Storage and Retrieval Systems, and Autonomous Guided Vehicles.
Automated Storage and Retrieval Systems (AS/RS) use robots and conveyors to move and retrieve materials in warehouses automatically. Autonomous Guided Vehicles (AGVs) navigate factory floors to transport materials without human guidance. Many modern factories deploy robotic systems to assist or replace humans in repetitive, heavy, or dangerous tasks.
Industrial robotics are programmable machines designed to handle material, assemble parts, and perform dangerous or repetitive tasks with extreme precision. Industrial robotic arms can perform tasks such as spot-welding, painting, or electronic component assembly. These robotic systems are common in automotive, electronics, metals, packaging, food, beverage, building products, and consumer products manufacturing.
Automation Layer Table
| Automation layer | Main function | Typical systems or software | Common hardware form factors |
|---|---|---|---|
| Field devices | Sense and execute physical work | Sensors, actuators, drives, industrial robots, machine vision, CNC, conveyors | Sensors, cameras, servo drives, VFDs, robotic cells, AS/RS, AGVs |
| Control layer | Execute deterministic logic and motion | PLCs, PACs, motion controllers, programmable controllers | PLC cabinets, I/O racks, drive systems, control panels |
| HMI layer | Local operator control and visualization | HMI software, machine dashboards, browser HMIs | Industrial panel PC, HMI panel PC, fixed touchscreen terminal |
| SCADA layer | Supervisory monitoring, alarms, trends, and centralized control | SCADA systems, historians, alarm platforms | Windows panel PCs, control room workstations, rugged Windows tablets |
| MES layer | Work orders, quality, traceability, OEE, downtime codes | Manufacturing execution systems, manufacturing information systems | Panel PCs, rugged tablets, handheld barcode/RFID devices |
| ERP layer | Orders, finance, inventory, procurement, planning | ERP, business intelligence, enterprise databases | Office workstations, servers, cloud clients, tablets for approved access |
| Fully integrated factories, often linked with Industry 4.0, use networked systems to manage production processes centrally with minimal human involvement. Implementing automation transforms labor-intensive manufacturing environments into agile, digitized production hubs. Flexibility in automation systems allows for continuous, mixed production of various parts or products without downtime for reprogramming, and automated production lines can be reprogrammed to adapt to market demands or produce new product variations. |
For buyers, the key point is simple: each automation layer has different hardware needs. A PLC cabinet does not need the same device as a forklift terminal, and a machine HMI does not need the same form factor as a quality inspector’s rugged tablet.
PLC, HMI, SCADA, MES, and ERP: What Each One Does
In daily conversation, PLC, HMI, SCADA, MES, and ERP can overlap. In practice, data usually moves from sensor to PLC, from PLC to HMI or SCADA, from SCADA and shop-floor inputs to MES, and from MES to ERP.
Programmable logic controllers (PLCs) receive data from sensors and issue commands to direct machinery. PLCs and PACs control actuators, robotics, pneumatic systems, drives, and motion control. They use protocols such as Ethernet/IP, PROFINET, Modbus TCP, PROFIBUS, EtherCAT, and serial interfaces, depending on the age and design of the equipment.
HMIs are the local operator interfaces. An HMI lets workers start or stop machines, change recipes, acknowledge alarms, select modes, and view process status. Industrial panel PCs often run HMI software, browser-based dashboards, or local visualization clients.
Supervisory Control and Data Acquisition (SCADA) systems allow managers to monitor and control industrial equipment from a centralized interface. SCADA systems collect data from PLCs, display trends, log alarms, and support centralized supervision across a production area or full plant. Operators may access SCADA from a control room workstation, an industrial panel PC, or a rugged Windows tablet.
MES connects production data with operational context. MES handles work orders, scheduling, traceability, quality checks, downtime reasons, and OEE. MES clients often run on industrial panel PCs at fixed stations and rugged tablets for mobile shop-floor data capture.
ERP is the business planning layer. ERP handles orders, finance, procurement, inventory, and customer demand. ERP generally does not control machines directly; it exchanges production and planning data with MES and sometimes with reporting systems.
Compact comparison: PLCs control machines, HMIs let operators interact locally, SCADA supervises equipment across the plant, MES manages production execution and traceability, and ERP manages business planning above the factory floor.
Industrial automation platforms from vendors such as Rockwell Automation, Siemens, Schneider Electric, and others often provide software and control components. Kcosit’s role is different: Kcosit supplies rugged computing hardware that helps operators, maintenance teams, and supervisors interact with those automation systems where work actually happens.
Factory Automation Hardware Selection Matrix
| Device class | Best fit | Critical checks | Wrong-fit warning |
|---|---|---|---|
| PLC or industrial controller | Deterministic machine and process control | I/O, cycle time, safety architecture, protocol, environmental rating, lifecycle | A tablet or PC should not substitute for engineered control logic |
| HMI panel | Dedicated machine visualization and operator input | HMI software, screen, touch, mounting cutout, ingress protection, approvals | Limited fit for mobile work or broad PC applications |
| Industrial panel PC | Fixed SCADA, MES client, line dashboard, vision or PC-based application | CPU/RAM, OS, ports, cooling, panel/VESA mount, power, service access | May be unnecessarily complex for a simple dedicated HMI |
| Rugged Windows tablet | Mobile MES/SCADA client, PLC tools, diagnostics, engineering and maintenance | Application/driver compatibility, ports, battery, dock, security, update control | Not appropriate for unengineered direct safety control |
| Rugged Android tablet | Mobile forms, scanning, quality checks, inventory, work instructions | Android Enterprise, kiosk/MDM, app integration, scanner services, offline sync | Wrong fit for software that requires Windows drivers or desktop components |
| Rugged handheld | High-volume barcode/RFID and one-handed material workflows | Scan engine, trigger ergonomics, read range, wireless roaming, battery | Small screen limits drawings, dashboards, and complex forms |
| Vehicle-mounted computer | Forklift, tugger, AGV support, yard and material movement | Vehicle power, ignition behavior, vibration, mount, Wi-Fi roaming, scanner pairing | Fixed installation reduces handheld flexibility |
Where Industrial Panel PCs Fit in Factory Automation
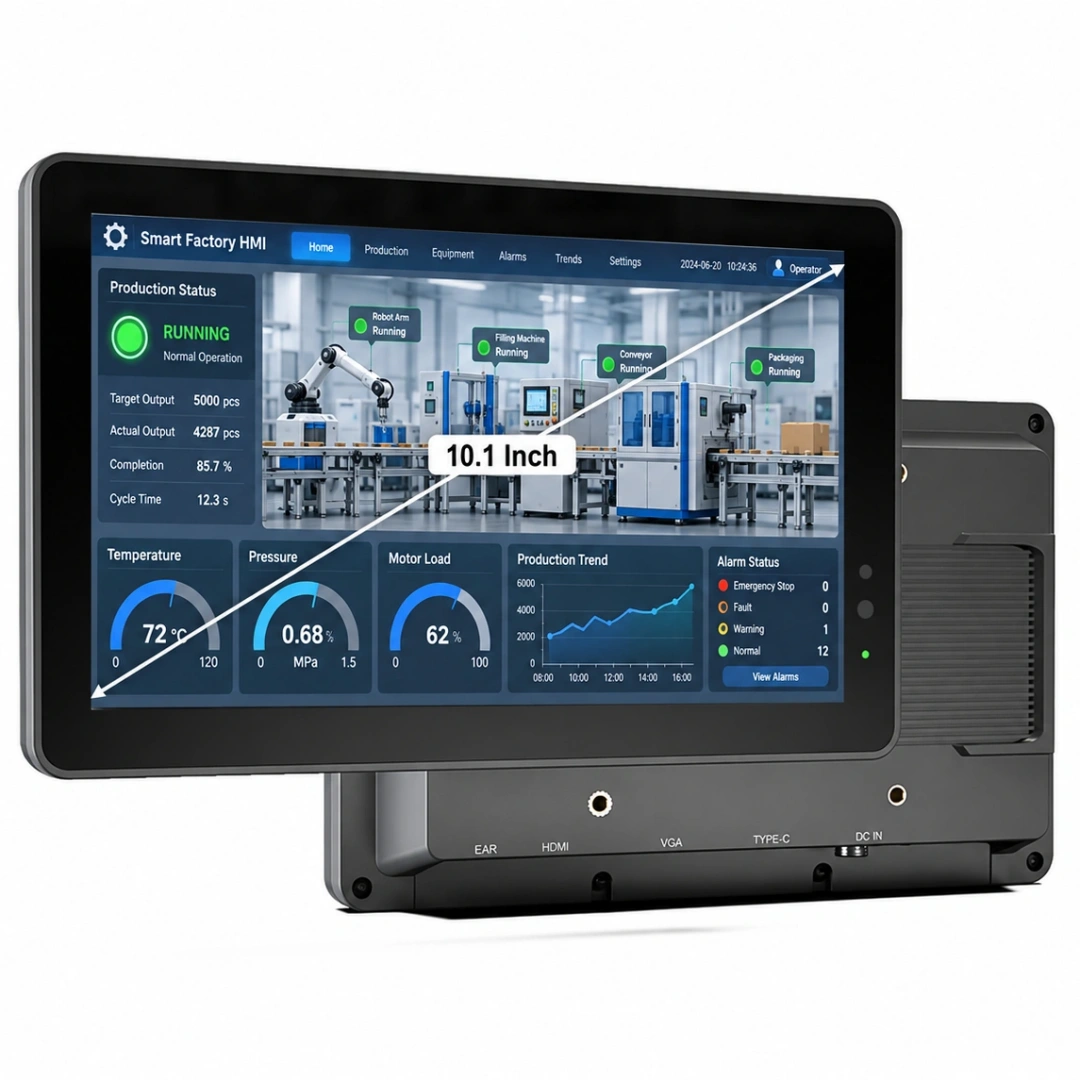
Industrial panel PCs and HMI panel PCs are fixed, always-on operator interfaces mounted on machines, panels, production cells, and line-side workstations. They are a practical fit where operators need stable local access to machine control, alarms, dashboards, and manufacturing information systems.
Common use cases include:
- Machine start/stop, mode selection, and local alarm acknowledgment
- Recipe management for packaging, filling, mixing, and food processing lines
- Monitoring CNC programs, cycle status, and tool alarms
- Displaying machine vision pass/fail results and camera status
- Showing line-level OEE, downtime, production count, and quality dashboards
- Supporting local SCADA or MES access at fixed stations
Industrial panel PCs are usually selected for fixed duty because they support permanent power, larger displays, rich I/O, and secure mounting. Mounting options include VESA mount, panel-mount bezels, swing arm systems, and machine enclosures. On the factory floor, vibration resistance and fanless design matter because moving fans can pull dust into a device and become a failure point.
Environmental requirements should be matched to the cell. A dry assembly station may need a lower ingress rating than a washdown food or beverage area. Buyers should evaluate IP rating, dust exposure, oil mist, splash risk, operating temperature, glove touch, wet-hand usability, sunlight-readable displays near dock doors, and cleaning procedures.
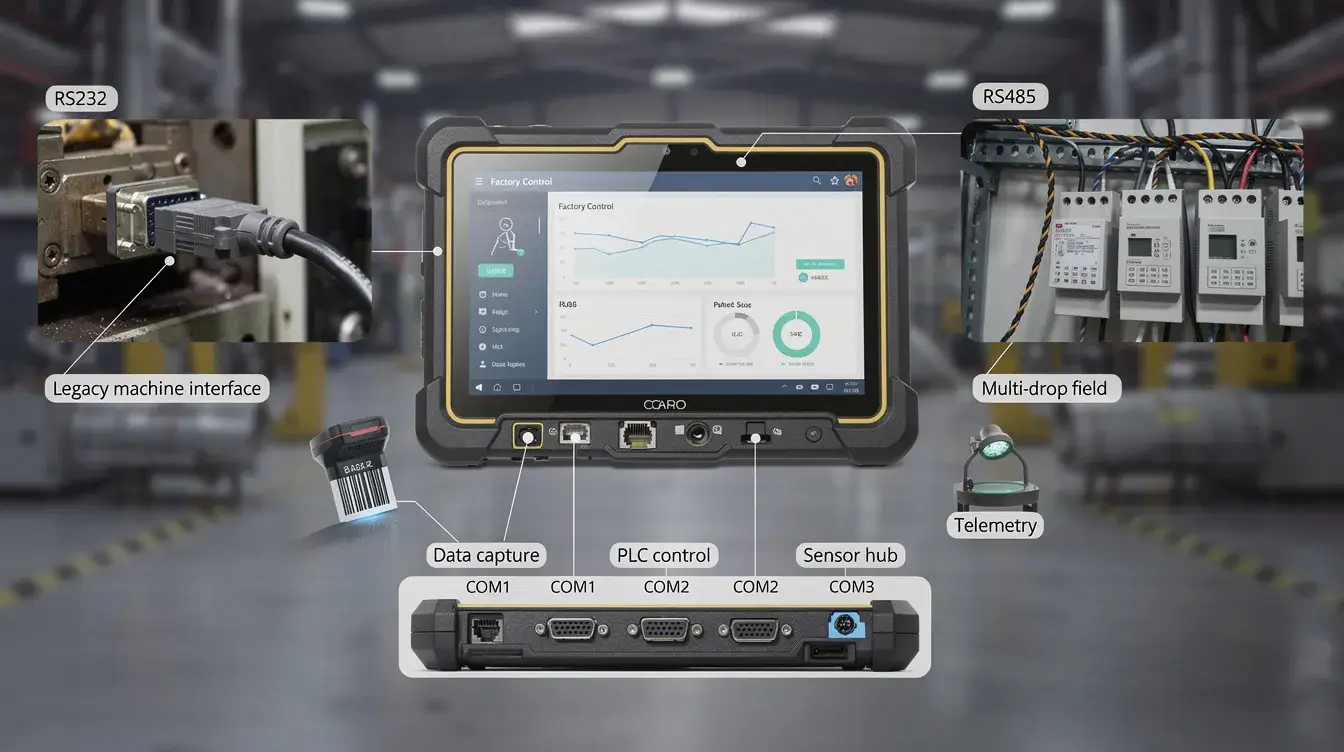
Kcosit industrial panel PCs for tough environments are positioned for fixed HMI points, line dashboards, and local machine interfaces. Depending on project configuration, industrial panel PCs can support Ethernet, USB, serial ports such as RS232 and RS485, and optional expansion such as CANbus or digital I/O through appropriate docking or expansion designs.
Device Role Matrix
| Factory role | Best-fit device | Why it fits |
|---|---|---|
| Machine HMI | Industrial panel PC or HMI panel PC | Fixed touchscreen, continuous power, strong mounting, local I/O |
| Line dashboard | Industrial panel PC | Larger display, always visible, suitable for OEE and alarms |
| Quality station | Panel PC or rugged tablet | Fixed checks use a panel PC; mobile sampling uses a rugged tablet |
| Packing station | Panel PC, rugged Android tablet, or handheld PDA | Depends on whether the worker is stationary or moving |
| Maintenance terminal | Rugged Windows tablet | Supports diagnostics, manuals, SCADA/MES clients, PLC tools |
| Forklift terminal | Vehicle-mounted rugged tablet | Docking, power, Wi-Fi, scanner support |
| Inventory and traceability | Rugged handheld PDA or barcode/RFID tablet | Fast scanning, RFID, NFC, mobile data capture |
A good device strategy does not force one form factor into every role. It assigns fixed devices to fixed work and mobile devices to mobile work.
Where Rugged Tablets Fit in Manufacturing Automation
Rugged tablets extend factory automation systems beyond fixed HMIs by enabling mobile workflows across maintenance, quality, logistics, and supervision. A rugged tablet for manufacturing is not a consumer tablet in a protective case; it is deployable industrial hardware built for drops, dust, vibration, long shifts, and real factory movement.
For maintenance, technicians use rugged Windows tablets to access PLC diagnostic tools, SCADA clients, digital manuals, drawings, work orders, and remote support applications beside the machine. This shortens troubleshooting time because the technician does not have to walk back to a control room or office PC.
For quality and inspection, operators can use rugged Android tablets with barcode scanners, UHF RFID, or NFC options to record measurements, capture photos, scan lots, and link results to MES records. This improves traceability and supports equipment effectiveness reporting because inspection results, downtime reasons, and operator input can be captured at the point of work.
For material handling, rugged tablets can be mounted on forklifts, carts, tuggers, and picking stations. They can guide pick/put-away tasks, scan pallets, update WMS or MES transactions, and communicate over Wi-Fi or Bluetooth-connected scanners. In a smart factory devices strategy, these mobile terminals connect production, warehouse, and logistics data.
Relevant mobile design features include MIL-STD-style shock resistance, IP-rated housings, glove touch, sunlight-readable displays, long battery life, hot-swappable batteries where required, secure vehicle docking stations, and charging accessories. Kcosit rugged tablets and industrial devices, including rugged Android tablets, rugged Windows tablets, vehicle-mounted tablets, handheld PDAs, barcode scanning tablets, UHF RFID devices, NFC-enabled tablets, GNSS/RTK rugged tablets, and docking station solutions, are designed for these B2B deployment workflows.

Hardware Requirements for Factory Floor Devices
The same PLC/HMI/SCADA/MES architecture can succeed or fail depending on whether the chosen devices survive the real environment. Factory hardware must tolerate dust, oil mist, humidity, washdown, vibration, shock, temperature swings, electrical noise, and continuous operation.
Environmental conditions drive device specifications. IP-rated protection helps prevent dust and water ingress. MIL-STD-style rugged design helps address drops, shock, and vibration. Fanless cooling reduces moving parts and helps prevent dust buildup. Solid-state storage is preferred over spinning disks in vibration-heavy areas.
Usability is equally important. Touchscreens should support glove and wet-hand operation where needed. Displays should be bright enough for dock doors, yards, or sunlight-exposed stations. Physical buttons may be needed for specific workflows, though emergency stop and safety circuits should remain part of certified machine safety design, not a tablet app.
Mechanical planning includes panel-mount versus VESA arm versus vehicle mount. Forklift and cart deployments often need docking stations for charging, secure mounting, power stability, and I/O expansion. Kcosit offers docking stations and mounting accessories for forklifts, carts, fixed workstations, and mobile deployment projects that align with its broader rugged tablet industry solutions across logistics, manufacturing, and other sectors.
Power and connectivity decisions also matter. Buyers may need DC-in, PoE in limited cases, wide-voltage vehicle power, Wi-Fi roaming, Bluetooth for peripherals, and optional 4G/5G when coverage is required between buildings or in yards.
Safety must be planned at the automation design level. Compliance with safety standards such as NEC, NFPA, ANSI B11, and ANSI/RIA 1506 is essential for ensuring machine and robot cell safety in factory automation systems. Safety guarding for factory lines must comply with OSHA and ANSI standards, which include features like locking and non-locking interlocked gates. Functional safety engineers play a critical role in integrating safety into the design of automation solutions, ensuring compliance with relevant safety standards, even in highly regulated environments such as those addressed by rugged tablets for the defense industry.
Spec-to-Risk Table
| Device specification | Operational risk if ignored |
|---|---|
| IP rating matched to dust, splash, or washdown | Water ingress, board corrosion, dust contamination, and early failure |
| MIL-STD-style drop and vibration resistance | Cracked displays, connector damage, and solder-joint failure |
| Fanless design | Fan failure, dust buildup, and overheating in dirty environments |
| Solid-state storage | Data loss or drive failure in vibration-heavy machine areas |
| Glove-capable touch | Slow operator input, missed alarms, unsafe workarounds |
| Sunlight-readable display | Poor visibility near dock doors, yards, and bright production areas |
| Hot-swappable or full-shift battery | Unplanned shutdowns during inspection, maintenance, or scanning |
| Industrial mounting or docking | Falls, cable strain, unsafe positioning, unstable power |
| Long-term platform availability | Revalidation costs when consumer models change unexpectedly |
The goal is not to buy the most rugged device for every station. The goal is to match the device to the actual risk.
Interfaces and Connectivity: LAN, USB, RS232, RS485, CANbus, Wi-Fi
Many factory device deployments fail because the selected panel PC or tablet lacks the right I/O. Automation environments often combine modern Ethernet equipment with legacy serial devices, specialized scanners, label printers, scales, drives, and robot controllers.
Ethernet/LAN is essential for SCADA, MES, OT networks, historians, and machine dashboards. Panel PCs may need dual LAN ports, gigabit Ethernet, VLAN support, or separation between machine networks and business networks. Rugged tablets may use Ethernet through docking stations when wireless is not acceptable.
RS232 and RS485 remain important. Many factories still depend on serial connections in 2026 for legacy PLCs, scales, labelers, barcode scanners, environmental controllers, and Modbus RTU devices. Removing serial ports from a project without checking the line can create expensive integration delays.
CANbus and fieldbus may be required for drive systems, motion control, mobile equipment, or specialized machine interfaces. Some deployments use gateways; others use docking stations or expansion modules to expose CAN interfaces to rugged devices.
USB and Bluetooth support scanners, label printers, external keyboards, measurement tools, cameras, and other peripherals. In industrial settings, buyers should consider connector strain relief, port covers, docking design, and whether the device will survive repeated plugging.
Wi-Fi is critical for mobile tablets and handhelds. Roaming configuration, access point density, interference, security, WPA3, 802.1X, and network segmentation should be validated before rollout. Optional cellular can support yards, remote buildings, and field service between sites.
Interface Requirement Matrix
| Equipment or workflow | LAN/Ethernet | RS232 | RS485 | CANbus | USB | Wi-Fi | Bluetooth |
|---|---|---|---|---|---|---|---|
| Modern PLC or SCADA client | Yes | Sometimes | Sometimes | Rare | Sometimes | Sometimes | Rare |
| Legacy PLC | Sometimes | Yes | Yes | Sometimes | Rare | Rare | Rare |
| Robot controller | Yes | Sometimes | Sometimes | Sometimes | Yes | Rare | Rare |
| Scale or weighing station | Sometimes | Yes | Yes | Rare | Sometimes | Rare | Rare |
| Label printer | Yes | Sometimes | Rare | Rare | Yes | Sometimes | Sometimes |
| Barcode scanner | Rare | Sometimes | Rare | Rare | Yes | Sometimes | Yes |
| Mobile forklift app | Through dock | Rare | Rare | Sometimes | Sometimes | Yes | Yes |
| Machine vision station | Yes | Rare | Rare | Rare | Yes | Sometimes | Rare |
A practical rule: document every machine, scanner, printer, scale, and network before choosing the device
Android vs Windows Devices for Factory Automation
Both Android and Windows are widely used in factory automation systems, but they fit different workflows.
Android is strong for app-based and browser-based tasks. Rugged Android tablets work well for mobile work orders, barcode scanning, RFID, NFC, quality checks, packing workflows, inventory counting, and lightweight MES or WMS clients. Android can also be easier for high-volume operator deployments, where the interface should be simple and controlled.
Windows is strong where the software stack requires full Windows compatibility. Rugged Windows tablets and Windows industrial panel PCs are common for SCADA clients, HMI software, PLC programming tools, diagnostics, engineering utilities, and legacy manufacturing applications.
Security and manageability should be planned with IT and OT together. Android fleets usually need mobile device management for factory tablets to control apps, patching, security policies, and remote wipe. Windows devices may require domain join, group policy, endpoint protection, patch management, remote support, and controlled update windows.
Many factories deploy a mixed fleet: Windows for engineering, maintenance, SCADA/MES access, and diagnostics; Android for high-volume operator tasks, scanning, inspection, and material handling, often relying on rugged tablets and durable devices for industry applications to standardize the hardware platform.
Android vs Windows Selection Matrix
| Use case | Android | Windows | Typical recommendation |
|---|---|---|---|
| SCADA client | Sometimes | Yes | Windows is preferred when full SCADA software is required |
| PLC programming | Rare | Yes | Windows preferred |
| Mobile work orders | Yes | Yes | Android for simple app workflows; Windows if CMMS requires it |
| Quality inspection | Yes | Yes | Android for guided forms and scanning; Windows for complex tools |
| Forklift terminal | Yes | Sometimes | Android often fits app-based WMS/MES terminals |
| Inventory counting | Yes | Sometimes | Android handhelds or tablets with barcode/RFID |
| Engineering diagnostics | Rare | Yes | Windows rugged tablet |
| Browser-based dashboard | Yes | Yes | Choose by environment, manageability, and peripherals |
The operating system decision should follow the application, not personal preference.
When a Consumer Tablet or Office PC Is Not Enough
Consumer-grade devices often look affordable at purchase time, but they can fail quickly under dust, vibration, temperature swings, shock, and 24/7 duty cycles on the factory floor. The visible device cost is only one part of the total cost; downtime, replacements, revalidation, broken mounts, and support effort can cost more.
Typical failure modes include cracked screens from drops, damaged ports from frequent plugging, overheating in sealed enclosures, Wi-Fi dropouts, battery swelling from constant charging, and inconsistent charging behavior on vehicles.
Consumer and office devices also have I/O gaps. They often lack native RS232, RS485, multiple LAN ports, CANbus options, wide-voltage power input, rugged docking, glove touch, and safe mounting for machines or vehicles.
Lifecycle is another issue. Consumer models change frequently, which makes it difficult to maintain validated configurations in a manufacturing automation system. Industrial buyers often need stable platforms, repeatable imaging, spare units, consistent accessories, and support across multiple sites.
Kcosit industrial and rugged devices are designed for repeatable B2B deployments where procurement teams, integrators, distributors, resellers, and OEM/ODM buyers need project-ready hardware rather than short-lifecycle consumer devices, whether for general factory use or specialized environments such as rugged tablets for the automotive industry.
Right-Fit/Wrong-Fit Table
| Use case | A consumer tablet or an office PC may be acceptable | Rugged industrial hardware is strongly recommended |
|---|---|---|
| Office analytics dashboard | Yes | Optional |
| Conference room production review | Yes | Optional |
| Supervisor’s desk near production | Sometimes | Recommended if exposed to dust or vibration |
| Machine HMI | No | Yes: industrial panel PC or HMI panel PC |
| Washdown food processing area | No | Yes: IP-rated industrial device |
| Forklift or tugger terminal | No | Yes: vehicle-mounted rugged tablet with dock |
| Welding cell or machining center | No | Yes: rugged, sealed, vibration-resistant hardware |
| Mobile quality inspection | Rare | Yes: rugged tablet with scanner/RFID/NFC options |
| Outdoor yard or dock | No | Yes: sunlight-readable rugged tablet |
| 24/7 line dashboard | No | Yes: fanless industrial panel PC |
If a device is tied to production, safety, output quality, or traceability, rugged industrial hardware is usually the safer procurement choice.
Factory Automation Device Pilot: Pass/Fail Tests
- Run the production application and required drivers with representative data.
- Test LAN, Wi-Fi roaming, USB, serial, scanner, printer, dock, and any gateway used by the workflow.
- Test power loss, battery depletion, restart, reconnect, queued records, and duplicate prevention.
- Operate the device with the intended gloves, cleaning process, mounting position, light, temperature, and shift length.
- Apply an OS, application, certificate, and security-policy update, then repeat the critical workflow.
- Replace a failed unit using the documented spare, enrollment, configuration, and data-recovery process.
Deployment Checklist for Factory Automation Devices
Even the right hardware can underperform without a structured deployment plan. Before scaling across a plant, run a limited pilot line or pilot area, then adjust mounting, radio settings, user interface design, accessories, and support processes.
Factory Automation Device Deployment Checklist
- Define the automation layer
- Field device, control, HMI, SCADA, MES, ERP, or mobile data capture
- Confirm whether the device is fixed, vehicle-mounted, handheld, or mobile
- Confirm software compatibility
- HMI software
- SCADA client
- MES or WMS client
- CMMS work orders
- PLC diagnostic or programming tools
- Browser requirements and authentication
- Verify I/O and protocol needs
- LAN/Ethernet
- USB
- RS232
- RS485
- CANbus
- Wi-Fi
- Bluetooth
- Barcode scanner, RFID, UHF RFID, NFC, GNSS/RTK if needed
- Specify mounting
- VESA mount
- Panel mount
- Arm mount
- Forklift dock
- Cart dock
- Wall mount
- Charging cradle
- Validate power
- AC adapter
- DC-in
- Wide-voltage vehicle power
- Battery duration
- Hot-swap requirement
- Charging location and spare battery strategy
- Match ruggedness to the environment
- IP rating
- Drop and vibration exposure
- Temperature range
- Oil, dust, splash, or washdown
- Screen cleaning procedure
- Test user experience
- Glove touch
- Wet-hand operation
- Stylus input if required
- Font size on dashboards
- Viewing angle
- Brightness at operator distance
- Validate wireless performance
- Wi-Fi coverage map
- Roaming between access points
- Interference near machinery
- Authentication
- OT network segmentation
- Optional cellular coverage
- Plan security and fleet management
- MDM for Android
- Domain join and policies for Windows
- Patch windows
- Remote support
- User access
- Asset tagging
- Lost-device process
- Plan spares and maintenance
- Spare ratio based on criticality
- Central charging
- Replacement docks and cables
- Battery health checks
- Storage health checks
- Cleaning procedures
- Documentation for operators and support teams
- Coordinate IT, OT, and production
- IT owns security and network standards
- OT owns automation compatibility
- Production validates workflow fit
- Maintenance validates serviceability
- Procurement validates lifecycle and supplier support
A successful rollout is usually staged. Pilot first, learn quickly, then scale during planned maintenance windows.

Final Procurement Summary: Choose Devices Around the Automation Layer
Successful factory automation systems align device selection with each automation layer and workflow. The goal is not to buy generic hardware; the goal is to choose devices that match the control architecture, factory environment, operator task, required interfaces, and support model.
Industrial panel PCs are usually best for machine HMI, line dashboards, fixed quality stations, and local SCADA clients. Rugged Windows tablets are often best for maintenance, engineering diagnostics, SCADA access, and full Windows industrial software. Rugged Android tablets fit inspection, mobile work orders, packing, scanning, and lightweight MES/WMS workflows. Rugged handheld PDAs and barcode/UHF RFID devices fit inventory, traceability, material handling, and fast shop-floor scanning.
Evaluate every purchase against six pillars:
- Automation layer
- Workflow and user role
- Environment and ruggedness
- Interfaces and connectivity
- Android vs Windows software fit
- Lifecycle, deployment support, and accessories
Kcosit supports these deployment patterns with industrial panel PCs, rugged Android tablets, rugged Windows tablets, rugged handhelds, barcode/RFID devices, vehicle-mounted tablets, and docking station solutions. For a practical next step, document your current PLC/HMI/SCADA/MES stack, map each device need to the matrices above, and contact Kcosit for hardware recommendations tailored to your specific factory automation system.
A final note on terminology: some searches for more factory automation systems, factory automation systems inc, full service systems integrator, full service, provides turnkey, turnkey automation solutions, solutions to manufacturing companies, manufacturing companies across diverse industries, company, inc, customers, partners, team, employees, founded, links, youtube, account, sign, week, meet, experts, and more jobs may point to specific integrators or job listings. For procurement, focus less on a name match and more on the system requirements: machines, production data, automation controls, drive systems, safety, implementation, process efficiency, costs, quality, support, and the workers who will use the devices every shift.
A factory tablet should be specified around the station, software, peripherals, network, and maintenance model. Use this guide to compare rugged tablet requirements before procurement and create a more complete device shortlist.
Factory Automation Architecture Sources
- ISA-95 / IEC 62264—enterprise-control integration and logical manufacturing-system levels.
- OPC UA overview and concepts—industrial information exchange and interoperability models.
FAQ
These FAQs address practical questions that automation engineers, maintenance managers, production supervisors, and procurement teams often ask after defining their factory automation architecture.
How do I phase device upgrades without disrupting production?
Start with one line, one cell, or one pilot area. Validate software compatibility, Wi-Fi coverage, I/O, mounting, charging, user workflows, and support procedures. After the pilot, roll out in stages during planned maintenance windows so production downtime stays controlled.
Can rugged tablets safely replace paper work orders and checklists?
Yes. Rugged Android or Windows tablets can integrate with MES, CMMS, WMS, or browser-based forms to deliver digital work orders, capture signatures, record photos, scan barcodes, add timestamps, and sync data over Wi-Fi. The key is to validate offline behavior, user permissions, and data accuracy before removing paper completely.
What is the best way to connect rugged devices to legacy PLCs?
Use devices, docks, or gateways that support the required interfaces, such as RS232, RS485, Ethernet, or Modbus. Many legacy PLCs and instruments still require serial configuration, so involve the systems integrator, controls engineer, or OT team before finalizing the tablet or panel PC specification.
How many spare devices should we keep on site?
For high-criticality roles, many plants plan roughly 5–10% spare capacity, adjusted by fleet size, repair time, and production impact. Keep spares charged, configured, asset-tagged, and ready to swap so a failed terminal does not stop a line or delay material handling.
Who should own mobile device management for factory tablets?
Ownership should be shared between IT and OT. IT should manage security, patching, identity, remote support, and MDM. OT and production should define approved apps, network access, usage rules, peripheral needs, and configurations aligned with factory automation requirements.